Golden Bake Advances Biscuit Factory Automation with Intelligent Ingredient Handling Systems
Golden Bake, the baking equipment division of EVERGROWING MACHINERY COMPANY LIMITED, showcased its latest biscuit production technologies at the 140th Canton Fair. The company highlighted an intelligent ingredient handling system through a detailed 3D production line model. The solution connects automated storage, ingredient dosing, pneumatic conveying, mixing, forming, and baking. It demonstrates how industrial automation can improve production consistency, workplace safety, and manufacturing efficiency.
Industrial Automation Connects Every Stage of Biscuit Production
At the 140th Canton Fair, Golden Bake presented an integrated approach to biscuit factory automation. Its system coordinates ingredient preparation with downstream production equipment. Therefore, manufacturers can manage material flow more efficiently and reduce interruptions between processing stages.The system addresses a common production challenge: delivering accurate ingredient quantities at the correct time. Manual handling often creates delays, weighing inconsistencies, and unnecessary dust exposure. Golden Bake combines automated material feeding and control systems to address these issues.The company's marketing manager highlighted three priorities: operational safety, product quality, and production efficiency. Intelligent ingredient handling helps reduce manual weighing errors and flour dust exposure. Moreover, coordinated production controls support more consistent manufacturing operations.
Automated Flour Handling Reduces Dust Exposure
Flour preparation involves several operations, including bag emptying, screening, conveying, and storage. Manual tipping can release airborne particles and increase contamination risks. Flour dust also presents a potential combustible dust hazard under certain conditions.Golden Bake integrates a bag-emptying station with a 30-mesh screening system. Dual-suction negative-pressure extraction captures airborne dust during material transfer. The feeding station handles up to 50 kg of flour per minute.A pulse-cleaned cartridge separator uses food-grade antistatic filter media. A rotary valve controls material discharge at the hopper outlet. Together, these components support continuous feeding while managing airborne flour particles.Pneumatic Conveying Supports Automated Material Storage
After screening, a pneumatic conveying system transfers flour through enclosed pipelines. The system can transport ingredients between different factory floors. This arrangement reduces manual material movement and supports centralized ingredient storage.The system includes a 1,000 kg buffer hopper. Gravity separation and filtration help control dust inside the storage unit. Meanwhile, intermittent bottom agitation helps prevent material bridging and discharge blockages.Golden Bake states that its powder handling and electrical systems follow the explosion-protection requirements of GB 50058-2014 and AQ 3009-2007. These design provisions address hazardous dust environments within the specified installation scope.Automated Ingredient Dosing Improves Recipe Consistency
Accurate ingredient measurement directly affects dough characteristics and finished biscuit quality. Variations in flour, sugar, and fat ratios can change water absorption and dough strength. Consequently, inconsistent dosing may affect biscuit thickness, texture, and forming performance.Golden Bake's automated dosing solution completes a weighing cycle in approximately three minutes. Its stated weighing accuracy reaches ±200 g. This capability helps manufacturers manage ingredient proportions during high-volume production.Different biscuit products require different ingredient sequences and processing parameters. Cookie production may prioritize the feeding order of sugar, fat, and flour. Cracker manufacturing may require staged mixing and fermentation.Therefore, manufacturers can configure the ingredient handling process according to their recipes and production equipment. This flexibility supports different biscuit manufacturing requirements without assuming identical processing conditions across product lines.Modular Factory Automation Supports Existing Production Lines
Many bakery manufacturers prefer upgrading existing facilities rather than replacing entire production lines. Industry survey figures reported by Baking Business indicate that 32% of surveyed bakery businesses focus on upgrades and retrofits. Another 22% plan to introduce additional equipment or production lines by 2026.Golden Bake offers a modular ingredient feeding system for existing biscuit manufacturing facilities. Engineers can adapt the configuration to factory layouts and installed equipment. This approach allows manufacturers to introduce automation without necessarily rebuilding their entire production infrastructure.For new factories and major capacity expansions, Golden Bake also provides turnkey biscuit production solutions. Its services cover facility planning, equipment arrangement, manufacturing, installation, and commissioning. This approach connects individual processing machines within a coordinated production environment.Biscuit Manufacturing Equipment and Integrated Production Solutions
Golden Bake presented several baking technologies at the 140th Canton Fair. These included a multifunctional cookie production machine and a cream puff production line.Its broader equipment portfolio also covers biscuit sandwich machines, biscuit creaming machines, and wafer stick machines. These machines serve different production processes and product requirements.When manufacturers combine ingredient preparation, mixing, forming, baking, and downstream handling, they can establish a more coordinated production line. Industrial control systems help manage equipment sequences and material movement. Depending on the project, PLC-based control architectures can support machine-level automation and process coordination.Digital Control Systems Support Production Efficiency
Biscuit manufacturers increasingly consider automation when improving overall equipment effectiveness (OEE). Coordinated equipment operation can help reduce material delays and production interruptions. In addition, digital monitoring can support production data collection and process analysis.Golden Bake continues to expand its international service network. The company aims to help customers improve equipment utilization and extend the service life of production assets.For larger manufacturing facilities, the integration of industrial automation, PLC control, and supervisory systems can support centralized production management. However, the final control architecture depends on the factory's equipment configuration and operational requirements.About Golden Bake
Golden Bake was established in 1999 by machine engineers and food processing specialists. The company manufactures equipment for industrial biscuit production and integrated baking facilities.Its product range supports cookies, soda crackers, Marie biscuits, and sandwich biscuits. The company also develops customized production systems covering ingredient preparation, forming, baking, cooling, and downstream automation.Golden Bake operates its own research and development center and manufacturing facilities. According to company information, it has installed more than 3,500 production lines across over 30 countries and regions. It also maintains long-term strategic partnerships with several international food manufacturers.
Industrial Automation in Megaprojects: Lessons in DCS Integration, Planning, and Delivery
Why Industrial Automation Determines Megaproject Success
Large industrial complexes demand more than advanced equipment and engineering expertise. They require coordinated industrial automation across process units, contractors, and operational teams. A failure in one interconnected unit can disrupt production elsewhere. Therefore, automation planning must address technical interfaces, project schedules, safety requirements, and long-term operations from the beginning.The Zhanjiang and Sadara chemical projects offer valuable lessons for delivering automation at scale. These projects demonstrate how early engineering involvement, consistent standards, and program-level coordination can reduce execution risks. They also show why successful delivery depends on both technical capability and disciplined management.The Iron Law of Project Management in Industrial Projects
Large projects frequently struggle to meet their original budgets, schedules, and performance targets. Research covering 16,000 projects across 136 countries highlights the scale of this challenge. According to the research cited in the original report, more than 91% exceeded their budgets, schedules, or both. Only one in 200 achieved all three intended outcomes: budget, schedule, and promised benefits.This pattern, known as the Iron Law of Project Management, creates a serious challenge for industrial automation programs. These programs involve complex control systems, long equipment lead times, multiple suppliers, and extensive site commissioning. Moreover, delays in automation can affect startup dates across entire production facilities.Project leaders must therefore address execution risks before construction accelerates. They need clear technical standards, defined responsibilities, realistic schedules, and effective communication between engineering teams. Early planning provides a practical foundation for controlling these interconnected risks.Zhanjiang: Integrating Automation Across 26 Chemical Plants
The Zhanjiang project applied lessons from Sadara while extending the use of digital engineering and smart manufacturing. The approximately $20 billion development includes 26 world-scale chemical plants within an integrated industrial complex. Its automation scope covers multiple production clusters and a broad range of process technologies.These facilities include a steam cracker, polyethylene production, ethylene oxide, ethylene glycol, and specialty chemicals. The project also combines proprietary BASF technologies with licensed process technologies. As a result, engineers must coordinate numerous interfaces across distributed control systems (DCS), safety instrumented systems (SIS), and manufacturing execution systems (MES).The challenge extends beyond installing individual control platforms. Teams must align instrumentation data, control strategies, alarm philosophies, and communication interfaces across different contractors. Consistent engineering practices help prevent separate plant units from developing incompatible designs.Digital Twins and Virtual Commissioning for Process Control
Digital engineering played an important role in Zhanjiang's automation strategy. Comprehensive digital twins supported virtual commissioning and operator training before actual production began. These capabilities allow engineering and operations teams to examine system behavior in a simulated environment.Virtual commissioning can help identify configuration issues and interface problems before equipment reaches the field. Meanwhile, operator training simulators give personnel opportunities to practice complex operating scenarios. These preparations can support a more controlled transition from construction to commissioning.However, simulation does not eliminate the need for physical testing. Engineers must still verify control logic, field-device interfaces, safety functions, and system performance. Combining digital models with structured acceptance testing creates a more complete verification process.Early FEED Involvement Improves Automation Delivery
The Zhanjiang execution program ran from 2019 to 2025. The main automation vendor (MAV) joined during the front-end engineering design (FEED) phase in 2021. This early involvement gave the team time to establish common engineering standards before large-scale deployment.The team could define hardware configurations, software conventions, functional specifications, and repeatable engineering procedures. It could also test field-device interoperability before mass procurement. These activities helped expose technical conflicts while design changes remained relatively manageable.Early engagement also supported a repeatable delivery model across multiple process units. Teams could develop prototypes, validate engineering concepts, and refine standards before scaling up production. Consequently, later units could benefit from lessons learned during earlier development and testing.Standardized DCS Engineering Reduces Rework
A standardized engineering approach helps automation teams manage complexity across large industrial programs. Instead of developing every plant unit independently, teams can reuse approved designs, configuration methods, and implementation standards. They can also apply consistent testing procedures across different contractors.A typical workflow begins with specification, design, prototyping, and certification during FEED. During execution, teams configure control applications, integrate third-party systems, assemble hardware, and conduct internal testing. Factory acceptance testing (FAT) then checks whether the equipment and applications meet defined requirements.Integrated factory acceptance tests provide another opportunity to verify interfaces across systems. After delivery, site teams continue with installation checks, commissioning, and operational verification. Each stage should follow documented acceptance criteria and clear responsibility assignments.This approach requires greater preparation during early engineering. However, it can reduce repeated design work, late changes, and avoidable testing failures. Teams can then focus more effort on planned execution rather than resolving preventable problems at the construction site.Program Management Connects Multiple EPC Contractors
Megaprojects need program management because individual project teams rarely control every technical and commercial interface. Program management coordinates related work packages around shared business and operational objectives. Project management, by contrast, focuses more directly on delivering a defined scope within agreed constraints.At Zhanjiang and Sadara, multiple engineering and construction contractors handled different plant clusters. Each contractor worked with its own schedules, specifications, and local requirements. The MAV program team therefore provided a central coordination function across these separate work packages.For example, instrumentation information from one contractor's piping and instrumentation diagrams (P&IDs) had to support another contractor's control-system engineering. Teams also needed consistent alarm principles, common engineering metrics, and aligned delivery schedules. Without this coordination, individual packages could meet their own targets while creating problems for the overall facility.A dedicated program team helps resolve these conflicts before they affect construction or commissioning. It maintains shared standards, coordinates technical decisions, and communicates changes across organizational boundaries. This structure also gives the owner a clearer view of overall progress and emerging risks.A Core Automation Team Maintains Engineering Standards
Standardization requires more than publishing technical documents. A dedicated core team must maintain standards, explain their application, and monitor compliance throughout the program. At Sadara, the core automation team performed three main functions.First, the team maintained implementation standards. It managed the standards library established during FEED and developed additional requirements when project needs changed. The team also consulted owners and EPC contractors before introducing revised standards.Second, the team supported engineering compliance. It explained procedures, answered technical questions, and reviewed requests for deviations. This process helped contractors understand common requirements while providing a structured route for handling exceptions.Third, the team coordinated execution. It aligned contractor schedules, monitored common performance indicators, and addressed cross-project dependencies. In addition, it helped simplify communication between individual engineering teams and the wider program.These responsibilities allow improvements from one plant unit to benefit other units. They also reduce the risk of inconsistent engineering decisions across a complex industrial site. As a result, standardization becomes an active management process rather than a static documentation exercise.Think Slowly During Planning and Act Quickly During Execution
A central lesson from these projects is the value of separating preparation from large-scale execution. During FEED, teams should invest time in resolving uncertainties, validating designs, and testing interfaces. Later, they can deploy proven solutions through repeatable processes.This principle is particularly relevant to PLC, DCS, SIS, and other industrial control systems. Unresolved interface questions can lead to software changes, hardware replacements, and repeated acceptance tests. These problems become more expensive when they emerge during construction or startup.Therefore, automation leaders should prioritize early technical reviews and clearly defined design responsibilities. They should also establish change-control procedures, interface registers, and measurable acceptance criteria. These practices support faster execution without sacrificing engineering discipline.Practical Lessons for Future Industrial Automation Projects
Future megaprojects can apply several lessons from Sadara and Zhanjiang. First, involve the main automation vendor during FEED whenever the project structure allows. Second, establish common hardware, software, and testing standards before expanding engineering across multiple units.Third, create a program-level team to coordinate contractors and resolve cross-package issues. Fourth, use digital twins and virtual commissioning where suitable, while retaining formal physical testing and acceptance procedures. Finally, track technical interfaces and schedule dependencies alongside cost and progress indicators.Industrial automation success depends on more than selecting capable control systems. It requires consistent engineering, early risk management, and coordination across the full project lifecycle. When teams prepare thoroughly and execute against shared standards, they can improve predictability and reduce avoidable rework.The experience of large chemical projects reinforces a practical conclusion: successful automation delivery begins long before equipment reaches the site. Strong planning, coordinated teams, and repeatable engineering processes provide the foundation for integrated industrial operations.
Industrial Automation Expands Materials Handling Portfolio with Two UK Acquisitions
Industrial Automation Strengthens Its Materials Handling Business
Axel Johnson International's Industrial Automation business unit has acquired two UK companies, Conveyor Units Ltd. and Bridge Bearings Ltd. The deal expands its presence in materials handling and complements its existing industrial businesses. Moreover, the acquisition broadens its portfolio of equipment and components for industrial automation and material transport systems.Conveyor Units Supports Factory Automation and Intralogistics
Conveyor Units designs and manufactures floor-based conveyor systems and related components. Its main customers include system integrators and original equipment manufacturers (OEMs). The company serves several industries, including manufacturing, warehousing, intralogistics and parcel handling. Its products support material movement across industrial facilities, distribution centers and automated handling operations. Therefore, the acquisition strengthens Industrial Automation's offering for businesses developing and maintaining material handling systems.Bridge Bearings Adds Industrial Bearing Products
Bridge Bearings supplies a broad range of bearings for industrial applications. Its product portfolio complements Conveyor Units' conveyor systems and associated components. Together, the two businesses offer Industrial Automation a wider selection of products for materials handling equipment. In addition, their combined capabilities may create opportunities to serve customers with related mechanical components and conveyor solutions.Two UK Sites Employ 145 People
Conveyor Units and Bridge Bearings employ 145 people across two locations in Stourport-on-Severn and Lye, United Kingdom. Both companies have established histories in the British industrial sector. Their experience and technical knowledge provide a foundation for continued development within Industrial Automation's broader business portfolio.A Combined History Dating Back to 1958
The businesses trace their origins to Edward Toye, who founded Bridge Bearings in 1958 and Conveyor Units in 1963. Ian Bytheway and Robert Hickman later took responsibility for the companies. They continued developing the businesses while maintaining the legacy established by their founder. Over time, both companies built established positions in their respective markets.Industrial Automation Sees Opportunities for Further Growth
Anton Kullh, Managing Director of Industrial Automation, highlighted the companies' reputations, skilled employees and technical expertise. He explained that their products complement the group's existing materials handling businesses. Furthermore, he sees opportunities to develop the companies through closer cooperation within the group.For industrial automation customers, this acquisition brings together conveyor equipment and bearing products under a larger industrial business group. However, the announcement does not specify changes to product lines, distribution arrangements or customer support. Further details on future integration plans remain unconfirmed.Existing Management Will Continue Leading the Businesses
Conveyor Units and Bridge Bearings will retain their existing management structure under Managing Director Liam Naven-Jones. The current leadership team will continue overseeing business operations and future development. Meanwhile, Ian Bytheway and Robert Hickman will support the transition to help maintain continuity.Robert Hickman described the ownership transition as an opportunity to build on the companies' existing progress. He emphasized the importance of finding a long-term owner with industrial experience and a commitment to future growth. The companies now enter their next development phase within Axel Johnson International's Industrial Automation business unit.What the Acquisition Means for Industrial Automation
The acquisition expands Industrial Automation's materials handling portfolio through two established UK suppliers. Conveyor Units contributes floor-based conveyor systems and components, while Bridge Bearings adds bearing products. Together, they strengthen the group's presence in equipment and components used across manufacturing, warehousing and intralogistics.For the wider industrial automation sector, the deal highlights continued investment in complementary industrial technologies and established component suppliers. Although PLC, DCS and other control systems support automated operations, this announcement focuses on materials handling equipment and mechanical components. The companies' continued operation under existing management also indicates an emphasis on business continuity during the transition.
Rockwell Automation Unveils FactoryTalk Conductor to Advance AI-Driven Industrial Automation
Introduction
Rockwell Automation has introduced FactoryTalk Conductor, an AI-native orchestration platform for industrial automation. The new software aims to coordinate artificial intelligence (AI) agents, engineering tools, data, and workflows across the automation lifecycle.The company announced the platform on October 21, 2026. It will make its public debut at Automation Fair 2026 in Boston. Rockwell Automation expects commercial availability in the first quarter of 2027.FactoryTalk Conductor targets manufacturers seeking to move beyond isolated AI applications. Instead, it connects multiple software environments to support coordinated engineering activities. As a result, industrial teams can explore more integrated approaches to system design, simulation, testing, and maintenance.How FactoryTalk Conductor Supports Industrial AI
Manufacturers increasingly use AI to improve engineering productivity and operational decision-making. However, separate AI assistants often handle individual tasks without coordinating broader workflows.FactoryTalk Conductor addresses this challenge through AI orchestration. Users can describe engineering tasks in natural language, while the platform connects relevant software tools, AI capabilities, and workflows.Moreover, this approach allows multiple AI agents to contribute to complex, multi-step activities. Engineers can therefore coordinate tasks across applications instead of managing each operation independently.According to Rockwell Automation's 2026 State of Smart Manufacturing Report, one-third of manufacturing operations already use AI to augment their activities. The company expects adoption to increase as manufacturers expand their AI deployments.Integration with PLC Programming and Engineering Software
FactoryTalk Conductor will initially integrate with four Rockwell Automation software products. These integrations cover several stages of PLC development, virtual commissioning, visualization, and engineering validation.The initial supported applications include:- Studio 5000 Logix Designer: Supports PLC programming and configuration for Logix-based control systems.
- Logix Echo: Provides controller emulation capabilities for virtual testing and validation.
- Emulate3D: Supports digital twin applications and simulation of industrial automation systems.
- FactoryTalk Optix: Provides tools for developing industrial visualization and operator interface applications.
Planned Expansion Across the Automation Lifecycle
Rockwell Automation plans to extend FactoryTalk Conductor across additional software applications. The roadmap includes FactoryTalk Design Studio, FactoryTalk Historian, Plex, and Fiix.These integrations could broaden AI-supported workflows beyond PLC engineering. For example, connections with industrial data platforms and maintenance software could support workflows involving operational information and equipment maintenance.Furthermore, broader software integration could help manufacturers connect engineering processes with production and asset management activities. This approach aligns with the industry's wider move toward connected factory automation and data-driven operations.The company has not yet confirmed a complete integration schedule for the additional products. Therefore, manufacturers should treat these connections as planned developments rather than currently available capabilities.AI Agents, Custom Skills, and Industrial Expertise
FactoryTalk Conductor combines Rockwell Automation-verified AI agents and skills with options for customer-developed capabilities. Organizations can create agents and skills tailored to their engineering standards, business requirements, and operational processes.This flexibility could help manufacturers adapt AI workflows to different control system architectures and production environments. In addition, verified capabilities provide a starting point for organizations that need industrial-specific functionality.Nevertheless, AI adoption in industrial environments requires careful validation. Engineering teams must consider application permissions, change management, cybersecurity, and functional safety requirements before deploying AI-generated actions in production systems.FactoryTalk Conductor's final deployment requirements and available safeguards will depend on the product's released capabilities and configuration options.Enterprise AI Governance and Language Model Flexibility
Industrial organizations often face strict requirements for data governance, cybersecurity, and technology management. FactoryTalk Conductor aims to accommodate different enterprise AI strategies through flexible language model options.According to the announcement, customers can use AI services hosted through FactoryTalk Hub or connect their preferred large language models and small language models. The platform also supports locally hosted open-weight models.Local model deployment may help some organizations manage data boundaries and reduce recurring token consumption costs. However, actual savings depend on hardware, infrastructure, model performance, and operating requirements.Consequently, manufacturers should assess model selection, access controls, data handling, and ongoing operating costs before choosing a deployment architecture.Key Benefits for PLC, DCS, and Factory Automation
FactoryTalk Conductor focuses on coordinating AI capabilities across industrial software rather than providing another standalone assistant. Its proposed benefits extend across several engineering and automation activities.1. More coordinated engineering workflowsThe platform connects supported applications to help teams organize design, development, simulation, and verification tasks.2. Reduced software workflow complexityAI orchestration may simplify multi-step activities that involve several engineering tools. As a result, engineers could spend less time coordinating separate applications manually.3. Flexible enterprise AI deploymentSupport for different language models gives organizations more options when aligning AI services with internal technology policies.4. Reusable industrial AI capabilitiesRockwell Automation-verified agents and customer-created skills can support repeatable workflows tailored to specific engineering requirements.5. Broader lifecycle integrationPlanned integrations could eventually connect PLC engineering, industrial data, production software, and maintenance processes within a more coordinated environment.These benefits describe the platform's intended direction. Actual productivity improvements will depend on implementation quality, supported workflows, system compatibility, and the accuracy of AI-generated results.FactoryTalk Conductor and the Future of Industrial Control Systems
AI orchestration represents a developing approach to industrial software integration. Traditional PLC and DCS architectures execute control logic through established engineering and runtime mechanisms. AI orchestration instead focuses on coordinating higher-level tasks across software tools, data sources, and engineering processes.These technologies can complement each other, but they serve different functions. FactoryTalk Conductor should not be confused with a PLC runtime, a DCS controller, or a replacement for established industrial control systems.For industrial users, the main opportunity lies in connecting engineering expertise with AI-assisted workflows. Nevertheless, manufacturers must preserve established validation procedures and retain appropriate human oversight, especially when changes affect live production or safety-related systems.As the platform develops, its practical value will depend on integration depth, governance controls, engineering accuracy, and support for real industrial use cases.Automation Fair 2026: First Public Demonstrations
Rockwell Automation plans to demonstrate FactoryTalk Conductor at Automation Fair 2026 in Boston. Attendees will be able to explore the platform through several exhibition experiences and dedicated technical sessions.The demonstrations will provide an opportunity to examine the platform's proposed role in AI-assisted industrial engineering. They may also help manufacturers understand how orchestration could fit into existing automation software environments.Commercial availability is expected in the first quarter of 2027. Until then, manufacturers should monitor official product announcements for confirmed specifications, licensing details, supported integrations, and deployment requirements.Frequently Asked Questions
What is FactoryTalk Conductor?FactoryTalk Conductor is an AI-native orchestration platform designed to coordinate AI agents, skills, software applications, and workflows across industrial engineering activities.How does FactoryTalk Conductor differ from a traditional AI copilot?A conventional AI copilot typically assists with individual tasks. FactoryTalk Conductor aims to coordinate multiple agents and software tools across broader, multi-step engineering workflows.Which Rockwell Automation products will it initially support?The initial integrations include Studio 5000 Logix Designer, Logix Echo, Emulate3D, and FactoryTalk Optix.Will FactoryTalk Conductor support other industrial software applications?Rockwell Automation plans to add FactoryTalk Design Studio, FactoryTalk Historian, Plex, and Fiix. The company has not confirmed a complete rollout schedule for these integrations.Can manufacturers create their own AI agents?Yes. The announced platform supports customer-created agents and skills alongside Rockwell Automation-verified capabilities.When will FactoryTalk Conductor become commercially available?Rockwell Automation expects commercial availability in the first quarter of 2027, following its public debut at Automation Fair 2026.Conclusion
FactoryTalk Conductor marks Rockwell Automation's move toward coordinated AI workflows across industrial engineering software. By connecting AI agents with PLC programming, simulation, visualization, and planned data integrations, the platform aims to support more integrated automation processes.Its success will depend on practical engineering capabilities, enterprise governance, and compatibility with existing industrial environments. For manufacturers exploring AI adoption, the platform offers a development to watch as industrial automation moves toward more connected and coordinated engineering workflows.
Siemens Targets 80% Factory Automation Through Industrial AI
AI Could Transform Industrial Automation
Siemens plans to increase factory automation to 70%–80% by applying artificial intelligence (AI) across manufacturing operations. The company currently estimates that automation covers approximately 30%–40% of factory production work. Cedrik Neike, a member of the Siemens Managing Board, believes AI can help close this gap. Moreover, the strategy could strengthen manufacturing competitiveness in Germany and other high-wage economies.The initiative combines industrial automation hardware, software, digital twins, and AI models. Together, these technologies aim to improve production efficiency while helping manufacturers maintain local operations.
Industrial Automation Faces Growing Productivity Pressure
Manufacturers in high-wage countries face rising labor costs and increasing international competition. Cedrik Neike estimates that factories must improve productivity by 7%–9% annually to remain competitive. However, conventional automation alone may not deliver these gains consistently across complex production environments.Therefore, Siemens sees AI as a way to accelerate factory modernization. Manufacturers can use intelligent control systems to optimize production sequences, reduce process interruptions, and improve resource utilization. In addition, AI-assisted analysis can help engineers identify bottlenecks and evaluate potential process improvements.For industrial facilities using PLC and DCS platforms, these developments could expand the role of data-driven optimization. Nevertheless, the actual benefits will depend on production requirements, equipment compatibility, and implementation quality.Digital Twins Support AI-Driven Factory Automation
Siemens and Nvidia are developing technologies that combine digital twins with AI models. A digital twin creates a virtual representation of a physical factory, production line, or industrial process. Engineers can use this virtual environment to examine operating conditions and test proposed changes before implementation.The approach reduces the need to experiment directly on production equipment. For example, engineers can simulate workflow adjustments, evaluate equipment interactions, and identify potential production constraints. They can then assess the results before introducing validated changes to the physical facility.Siemens contributes industrial software, automation equipment, and manufacturing data. Nvidia provides computing infrastructure, simulation technologies, and AI capabilities. Their collaboration focuses on physical AI, which enables AI systems to understand and interact with real-world environments.This approach could support more flexible factory automation. However, manufacturers still need accurate models, reliable operational data, and suitable engineering validation. AI recommendations must also comply with established machine safety requirements and industrial control procedures.PLC and DCS Systems in the Physical AI Era
The expansion of AI does not eliminate the need for established industrial control systems. PLCs continue to execute machine-level control logic, while DCS platforms coordinate processes across larger industrial installations. Both remain important components of modern manufacturing infrastructure.AI can complement these systems by analyzing operational data and identifying opportunities for improvement. For instance, manufacturers may combine historical production records, equipment condition data, and simulation results to refine operating strategies.However, engineers must distinguish between optimization functions and safety-critical control functions. AI-generated recommendations should not bypass validated control logic, protective interlocks, or established safety procedures. Instead, manufacturers should integrate AI through carefully designed interfaces and appropriate engineering reviews.Consequently, the future of industrial automation will likely combine conventional control systems with AI-based decision support. This model allows manufacturers to explore new capabilities without abandoning proven control architectures.Siemens Erlangen Campus: A Manufacturing Investment Through 2030
Siemens is investing €500 million to expand its Erlangen site by 2030. The development includes a technology campus, an innovation center, and additional production capacity. The company plans to strengthen its position in power electronics while expanding its AI-driven manufacturing capabilities.The existing Erlangen facility also provides a practical environment for testing digital manufacturing technologies. Siemens reports that AI, digital twins, and robotics have contributed to a 69% productivity increase and a 42% reduction in energy consumption.These figures illustrate the potential impact of coordinated digitalization. However, manufacturers should evaluate such results against their own production conditions, baseline measurements, and investment requirements.Siemens also reports more than 100 AI applications at the site. These applications demonstrate how manufacturers can introduce AI across multiple operational areas rather than treating it as a single automation project.Power Electronics and Energy Transition Manufacturing
Power electronics play an important role in electrification, renewable energy integration, and modern power conversion systems. Siemens intends to expand its manufacturing capabilities in this area through its Erlangen investment.The initiative also connects factory automation with broader industrial energy objectives. More efficient production processes can help manufacturers manage energy consumption while increasing output. In addition, digital twins can help engineers evaluate production changes before committing resources to physical modifications.For manufacturers supplying electrical infrastructure and energy technology, these capabilities may support more responsive production planning. Nevertheless, output quality, product traceability, and process stability remain important performance requirements.Automation Targets Raise Questions About Manufacturing Jobs
Siemens' automation strategy also raises questions about employment. In March 2025, the company announced plans to cut 5,600 jobs in its factory automation business by late 2027. The announcement included approximately 2,600 positions in Germany.This context highlights a central challenge for industrial manufacturers. Automation can help retain production in high-cost economies, but it can also reduce demand for certain tasks. The overall employment impact depends on investment decisions, production growth, workforce skills, and the creation of new technical roles.Therefore, companies pursuing higher automation levels must consider workforce development alongside technology deployment. Training in industrial software, robotics, data analysis, and AI integration could help employees adapt to changing production requirements.Labor representatives will likely assess Siemens' 80% automation target through its practical effects on staffing, job quality, and long-term manufacturing investment.The Global Race for Physical AI
Siemens and Nvidia are not alone in pursuing AI technologies for physical operations. Robotics developers are also exploring AI models that help machines perform tasks in changing environments. These developments include synthetic training data, spatial sensing, and foundation models for robotic manipulation.Synthetic data can help developers generate training scenarios without collecting every example from physical equipment. Meanwhile, spatial sensors provide information about surrounding objects and environmental conditions. Foundation models can help robots interpret tasks and coordinate movements.These technologies may eventually support more adaptable industrial robots and automated production lines. However, practical deployment still requires appropriate sensing, motion control, system integration, and safety validation.For industrial automation suppliers, the wider trend creates opportunities across control hardware, industrial networking, sensors, simulation software, and intelligent robotics. Manufacturers will need to assess how these technologies fit existing PLC, DCS, and supervisory control architectures.What Siemens' 80% Automation Goal Means for Manufacturers
Siemens' target reflects a broader shift from conventional automation toward AI-assisted industrial operations. Digital twins can help engineers test changes, while AI models can support analysis and process optimization. Meanwhile, established PLC and DCS platforms will continue to manage deterministic control and essential process functions.However, a higher automation percentage does not automatically guarantee better productivity. Manufacturers must also consider capital costs, equipment integration, cybersecurity, workforce training, and measurable operational results.The most practical strategy is to introduce AI where it addresses clearly defined production problems. Companies can begin with simulation, predictive analysis, and workflow optimization before expanding into more complex applications.Ultimately, Siemens' Erlangen project offers a useful example of how industrial automation and physical AI may develop together. Its long-term impact will depend on whether manufacturers can translate these technologies into measurable productivity gains while maintaining safe operations and sustainable employment.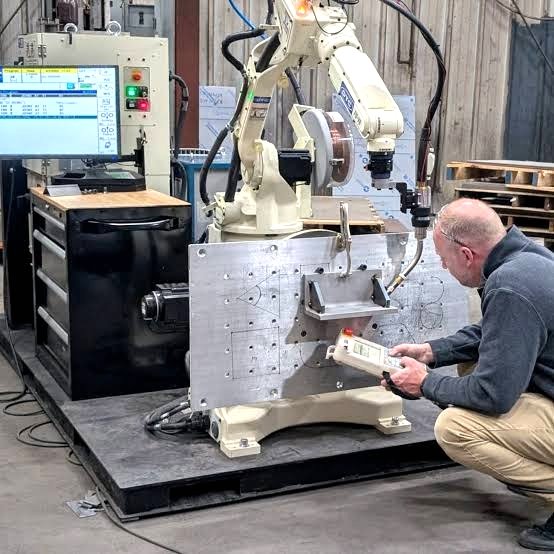
Capital Machine Acquires KC Robotics to Expand Industrial Automation Capabilities
Capital Machine Expands Its Industrial Automation Business
Capital Machine has acquired KC Robotics, an industrial robotic systems integrator based in West Chester, Ohio. The acquisition expands Capital Machine’s industrial automation capabilities and strengthens its position in engineered manufacturing systems. The companies have not disclosed the financial terms.This transaction marks Capital Machine’s first add-on acquisition since partnering with Rotunda Capital Partners in March 2025. Moreover, it supports a broader strategy to deliver complete automation solutions. Manufacturers can combine machinery, engineering, system integration, installation and ongoing technical support through one supplier.KC Robotics Brings More Than 35 Years of Robotics Expertise
KC Robotics has over 35 years of experience designing and integrating custom robotic automation systems. The company serves manufacturers across North America with solutions for welding, cutting, finishing, material handling, machine tending, assembly and machine vision.Its in-house capabilities include engineering, fabrication and robot programming. In addition, KC Robotics holds integration credentials from major industrial automation suppliers, including FANUC, ABB, Yaskawa Motoman, KUKA, Fronius, ESAB and Miller. These capabilities support projects that require coordinated robotics, production equipment and application-specific engineering.Integrated Automation Connects Machinery and Control Systems
Capital Machine distributes and services metal fabrication equipment, including press brakes, metal cutting machinery and robotic welding systems. The company operates showrooms in Tampa, Atlanta, Dallas, Indianapolis and Harrisburg. Its field service network also covers 22 states.By integrating KC Robotics, Capital Machine can address more stages of an automation project. Customers can work with one provider to define requirements, select equipment, engineer robotic cells and coordinate installation.This approach can reduce the coordination burden associated with separate equipment suppliers and system integrators. Furthermore, integrated projects can align robot programming, machine interfaces, production processes and operator requirements more effectively. PLC-based control systems may also form part of these projects, depending on each application's technical scope.
Capital Machine Targets Growing Factory Automation Needs
Manufacturers increasingly seek automation solutions that extend beyond individual machines. They need systems that support production efficiency, consistent processes and changing manufacturing requirements.Dan DeBickero, CEO of Capital Machine, highlighted this shift in customer demand. He explained that KC Robotics brings the engineering expertise needed to design and deliver complete automation systems. Meanwhile, Capital Machine contributes its equipment portfolio and aftermarket service capabilities.Together, the companies aim to provide a more coordinated route from equipment selection to automation implementation. As a result, manufacturers can access machinery, robotic integration and ongoing support through a broader service offering.KC Robotics Retains Its Brand and Existing Team
KC Robotics will continue operating under its current name within Capital Machine. Kyle Carrier will remain in leadership, and customers can continue working with their existing engineering and project management teams.In addition, KC Robotics customers gain access to Capital Machine’s wider equipment range and aftermarket service network. This structure preserves established customer relationships while expanding the resources available for future projects.Kyle Carrier, CEO of KC Robotics, said the combination would help the company reach more manufacturers. He also emphasized the value of Capital Machine’s service network and broader business resources. Therefore, the acquisition combines KC Robotics’ specialist integration expertise with Capital Machine’s established machinery business.What the Acquisition Means for Industrial Automation
Capital Machine has supplied and serviced metal fabrication machinery since 1984. Its portfolio includes press brakes, metal cutting equipment and robotic welding systems. The acquisition adds further engineering and robotic integration capabilities to this established business.For manufacturers, the combined offering could simplify the delivery of factory automation projects. However, the technical benefits will depend on each project's requirements, system design and implementation.The acquisition also reflects a wider industrial automation trend. Equipment suppliers increasingly combine machinery, robotics, control systems and lifecycle services to meet manufacturers' project needs. For facilities planning new production lines or upgrading existing equipment, integrated engineering support can help coordinate multiple technologies within one manufacturing environment.As industrial automation requirements continue to evolve, the combination positions Capital Machine and KC Robotics to pursue projects that require both fabrication equipment and custom robotic systems.
Yorkshire Engineering Firm Introduces Robotics Rental for Industrial Automation Trials
Robotics rental targets factory automation investment uncertainty
Yorkshire-based Total Automated Solutions (TAS) has launched a robotics Proof-of-Concept Rental Service. The service helps manufacturers test robotic automation before making major capital investments.TAS operates from Tockwith, between York and Wetherby. The company provides industrial automation, electrical engineering, control systems, and systems integration services across the UK.For many manufacturers, the technical feasibility of robotics does not guarantee a strong business case. Production teams must also verify productivity, quality, safety, labor requirements, and operating costs.The new rental model addresses this evaluation challenge. Manufacturers can test a configured robotic system under real production conditions before committing to permanent deployment.Industrial automation trials use real production conditions
Customers can typically rent a robotic solution for two to six months. TAS can install the system at the customer's facility or test it within its own workshop.This approach gives engineering teams access to practical production data. Moreover, teams can evaluate cycle times, product handling, process consistency, and operator interaction.TAS engineers assess the application before configuring the robotic system. They can also program the robot and integrate suitable grippers, guarding, and safety systems.As a result, manufacturers can evaluate the complete automation concept rather than testing the robot alone.Robotics supports multiple factory automation applications
The rental service targets repetitive and labor-intensive production processes. Potential applications include:- Repetitive product handling
- Pick-and-place operations
- Machine loading and unloading
- Packing and palletizing
- Production process support
- Ergonomically demanding tasks
- Applications involving workplace safety risks
- Production bottlenecks
PLC and control systems remain important integration points
A robotic cell rarely operates as an isolated machine. In many industrial automation projects, the robot interacts with PLC control systems, machine interfaces, safety equipment, and production equipment.The PLC may coordinate machine states, interlocks, sensors, and robot signals. Industrial communications can also connect robotic equipment with existing control architectures.For larger production systems, SCADA platforms can provide additional process monitoring and production data. DCS platforms may also interact with robotic equipment in process industries, depending on the application.Therefore, a proof-of-concept should consider the complete control architecture. Testing only the robot's movement may overlook important integration constraints.Safety engineering must accompany robotics deployment
Industrial robot trials also require appropriate attention to machine safety. Guarding, safety devices, access control, and emergency-stop functions can affect the final cell design.The exact safety architecture depends on the application, equipment, and site requirements. Manufacturers should therefore assess the complete workcell rather than treating the robot as a standalone device.This consideration becomes particularly important when robots operate near production personnel. A rental trial can reveal practical issues that may not appear during an initial engineering assessment.Proof-of-concept data can support capital investment decisions
Kevin Chapman, Owner and Managing Director responsible for Robotics Rental at TAS, said manufacturers often need greater certainty before investing in robotics.A concept can look technically suitable during an initial assessment. However, production data provides a stronger basis for evaluating the proposed solution.The trial therefore creates an opportunity to measure actual results. Manufacturers can examine productivity, quality, workforce deployment, and process compatibility.At the end of the rental period, customers can choose their next step. They may purchase the system, develop a permanent robotic cell, or reconsider the application.Robotics rental may benefit smaller manufacturers
Small and medium-sized manufacturers often face tighter capital budgets than large industrial organizations. Consequently, a rental-based evaluation can reduce the commitment required during the initial assessment stage.The model also gives production and engineering teams time to understand the technology. They can identify process changes before implementing a permanent automation solution.From an industrial automation perspective, this staged approach can also expose integration requirements earlier. Teams can determine how robotics will interact with existing PLCs, control systems, machines, and operators.Yorkshire strengthens its industrial automation ecosystem
TAS's new service adds another robotics capability to Yorkshire's manufacturing and engineering landscape. The region has a broad industrial base covering manufacturing, engineering, automation, and related technologies.Moreover, robotics adoption increasingly connects with wider factory automation strategies. Manufacturers may combine robots with PLC systems, machine vision, industrial networks, SCADA, and data platforms.The practical challenge remains application engineering. Selecting a robot represents only one part of a successful automation project.Existing automation services support permanent deployment
The robotics rental service complements TAS's existing engineering capabilities. These include control panel and MCC manufacture, PLC and SCADA software, electrical installation, industrial communications, and systems integration.This combination can support a transition from an initial proof of concept to a permanent production installation.In practical projects, that transition requires more than demonstrating robot motion. Engineers must also address electrical interfaces, control logic, safety functions, communications, mechanical integration, and production requirements.Application scenario: testing machine loading automation
Consider a manufacturer that manually loads components into a production machine. The company may understand the potential value of robotic handling but lack sufficient production data.A rental cell could reproduce the loading process within the actual production environment. Engineers could then monitor the robot's interaction with the machine and surrounding equipment.The manufacturer could compare the trial against its existing process. Relevant measurements might include cycle performance, operator involvement, production flow, and process consistency.If the results support further investment, the company could then develop a permanent factory automation solution based on measured requirements.Industry perspective: automation evaluation is becoming more data-driven
Robotics projects increasingly require both engineering validation and commercial justification. A robot can perform a task successfully while still failing to deliver the expected production value.Therefore, proof-of-concept testing has an important role in industrial automation planning. It connects technical feasibility with real operating conditions and measurable production results.For manufacturers considering robotics, the most useful trial is not necessarily the most sophisticated one. Instead, the trial should reproduce the target process accurately and generate meaningful operational data.
Rockwell Automation Valuation: Can Cash Flow Support Its Industrial Automation Growth?
Rockwell Automation remains a major name in global industrial automation and control systems. Its share price has also delivered a strong multi-year increase.The stock recently traded around US$415.62. That valuation raises an important question about future cash generation.Investors now need to examine whether Rockwell Automation's cash flow can support current market expectations. The company's position across PLC, industrial software, control systems, and factory automation also adds another layer to this discussion.
Rockwell Automation's Strong Share Price Performance
Rockwell Automation has generated a 55.2% share price return over the past three years. That performance has increased expectations for future business growth.However, share price appreciation does not automatically indicate stronger underlying cash generation. Investors therefore need to compare market valuation with operating performance.Rockwell Automation generates revenue from industrial automation hardware and software. Its portfolio includes programmable automation, control platforms, information systems, and factory automation technologies.These businesses serve manufacturers that increasingly connect machines, PLCs, production systems, and industrial software. As a result, automation demand can influence both revenue growth and future cash generation.Free Cash Flow Provides a Different Valuation Perspective
Free cash flow offers another way to examine Rockwell Automation's valuation. The latest twelve-month figure cited in the source stands near US$1.5 billion.A DCF model uses expected future free cash flow to estimate intrinsic business value. Therefore, the assumptions behind future cash generation strongly influence the result.The current DCF analysis still produces a value below the reported US$415.62 share price. This difference suggests that the market already reflects substantial expectations for future growth.However, DCF models remain sensitive to assumptions about revenue, margins, capital spending, and long-term growth. Small changes in these inputs can materially affect the estimated value.Industrial Automation Software Changes the Growth Equation
Rockwell Automation operates in a market that increasingly combines physical control equipment with industrial software.Modern factories connect PLCs, distributed control functions, industrial networks, drives, sensors, manufacturing software, and data platforms. These systems generate large amounts of operational data.Industrial customers increasingly use this data for predictive maintenance, production optimization, cybersecurity, and process improvement. Therefore, software can become an increasingly important part of automation investment.Rockwell Automation's work with Anthropic's Project Glasswing also highlights growing interest in AI-enabled industrial cybersecurity. The source links this work with expectations for stronger demand for secure industrial software.However, future AI-related revenue still depends on commercial adoption and actual customer spending. Market expectations should therefore remain separate from confirmed cash generation.AI and Cybersecurity Add New Opportunities for Control Systems
Industrial cybersecurity has become closely connected with factory automation and control systems.Manufacturers must protect PLCs, industrial networks, engineering workstations, remote-access systems, and production data. Cybersecurity risks can affect both information technology and operational technology environments.AI may help organizations detect abnormal system behavior and respond to emerging cyber threats. However, industrial environments impose stricter requirements than many conventional IT applications.Control-system engineers must consider system availability, deterministic communication, safety requirements, legacy equipment, and operational continuity. These factors can slow technology adoption compared with consumer or general enterprise software.Rockwell Automation's exposure to industrial software therefore provides potential growth opportunities. At the same time, investors must determine how quickly those opportunities can translate into measurable cash flow.PLC and Factory Automation Demand Remains Important
Rockwell Automation's valuation should also be viewed within the broader industrial automation cycle.PLC platforms remain central to discrete manufacturing applications. Engineers use PLCs to coordinate sensors, actuators, motors, drives, robots, and machine-level sequences.At larger production sites, PLC systems often interact with supervisory software, SCADA platforms, manufacturing execution systems, and enterprise applications.This layered architecture creates opportunities for automation suppliers to expand beyond hardware. Software subscriptions, analytics, cybersecurity, and lifecycle services can provide additional revenue streams.Nevertheless, industrial capital expenditure can fluctuate with economic conditions. Manufacturers may postpone automation projects when production demand or investment budgets weaken.DCS, Control Systems, and Software Create Longer-Term Opportunities
The wider automation market also includes DCS platforms, process control, safety systems, and machinery monitoring.These technologies support industries such as energy, chemicals, pharmaceuticals, food processing, and utilities. Their investment cycles often differ from those in discrete manufacturing.Rockwell Automation therefore competes within a broad control-system ecosystem. Customers increasingly expect automation platforms to communicate across production levels.This trend favors integrated architectures that combine control hardware, industrial networking, data management, cybersecurity, and software. However, integration also increases technical complexity and implementation requirements.From an engineering perspective, the strongest automation platforms are not defined only by hardware specifications. Long-term support, system compatibility, engineering tools, cybersecurity, and lifecycle management also influence purchasing decisions.What Could Support the Current Valuation?
The current market valuation appears to depend partly on expectations for continued industrial automation growth.Several factors could influence that outlook. These include factory modernization, industrial software adoption, cybersecurity spending, AI applications, and increasing automation across manufacturing facilities.Rockwell Automation's established position in industrial control and automation gives it exposure to these trends.However, these opportunities do not automatically translate into future free cash flow. Investors still need to monitor revenue growth, operating margins, capital requirements, and actual cash conversion.The difference between an attractive technology narrative and measurable financial performance remains important when assessing valuation.What Industrial Automation Engineers Should Watch
From an engineering perspective, several developments deserve attention.First, manufacturers continue moving from isolated automation islands toward connected production architectures. This trend increases demand for industrial communication and data integration.Second, cybersecurity increasingly affects PLC, DCS, SCADA, and industrial network design. Security requirements now influence system architecture from the initial engineering stage.Third, AI may introduce new functions around predictive maintenance, anomaly detection, engineering assistance, and industrial data analysis.Finally, customers continue seeking longer equipment lifecycles and simpler system integration. Automation suppliers must therefore support both new digital technologies and installed legacy systems.These technical trends could influence future demand. However, the financial impact depends on customer adoption and the supplier's ability to convert demand into sustainable cash flow.Practical Factory Automation Scenario
Consider a large manufacturing facility upgrading an existing production line.Engineers may replace legacy PLC hardware while retaining motors, sensors, drives, and field instrumentation. The new control system can then connect production data with higher-level software.The project may also introduce industrial cybersecurity controls and remote diagnostics. AI-based analytics could later analyze machine and production data.This approach illustrates how automation spending can expand from hardware replacement into software and services. It also explains why industrial automation companies increasingly position themselves as technology platforms rather than hardware suppliers alone.A Balanced View of Rockwell Automation's Valuation
Rockwell Automation sits at the intersection of industrial automation, PLC control, factory software, industrial cybersecurity, and emerging AI applications.Its 55.2% three-year share price return has raised the financial expectations surrounding the company. Meanwhile, the cited US$1.5 billion trailing free cash flow provides an important reference point.The DCF analysis discussed here places estimated intrinsic value below the reported US$415.62 share price. Therefore, the market appears to require substantial future business performance to support the current valuation.At the same time, industrial software, cybersecurity, factory modernization, and AI could create additional long-term opportunities.The key issue is execution. Investors and industry observers should compare future automation demand with actual revenue growth, margins, and free cash generation.For the industrial automation sector, that distinction matters. Technology adoption can create significant opportunities, but financial results ultimately determine how much economic value those opportunities produce.